Integrated Ship Panel Production Line Automation: Building Connected Workflows in Shipyard Fabrication
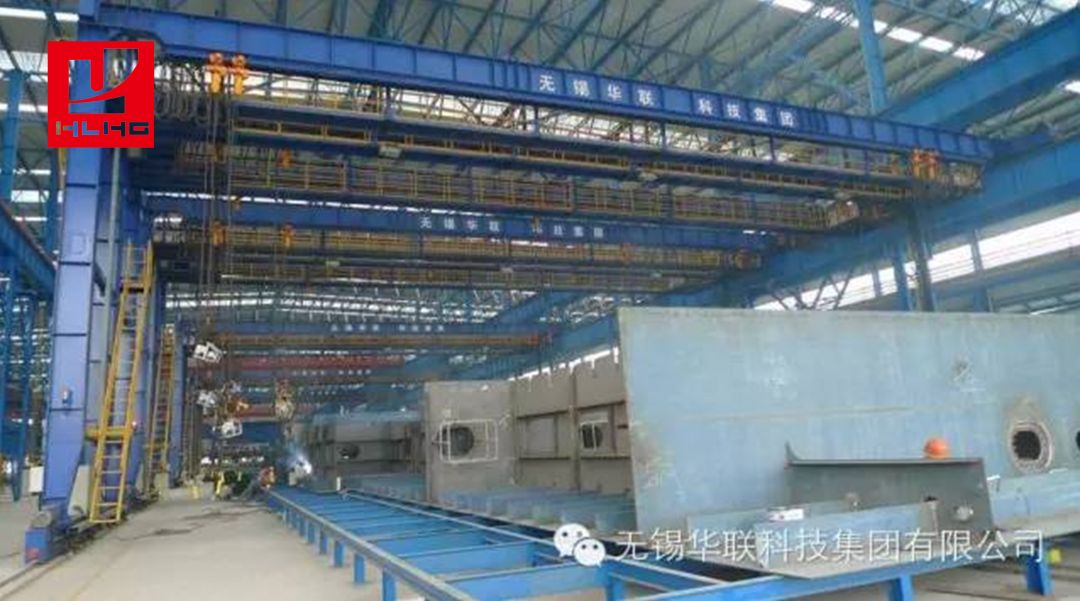
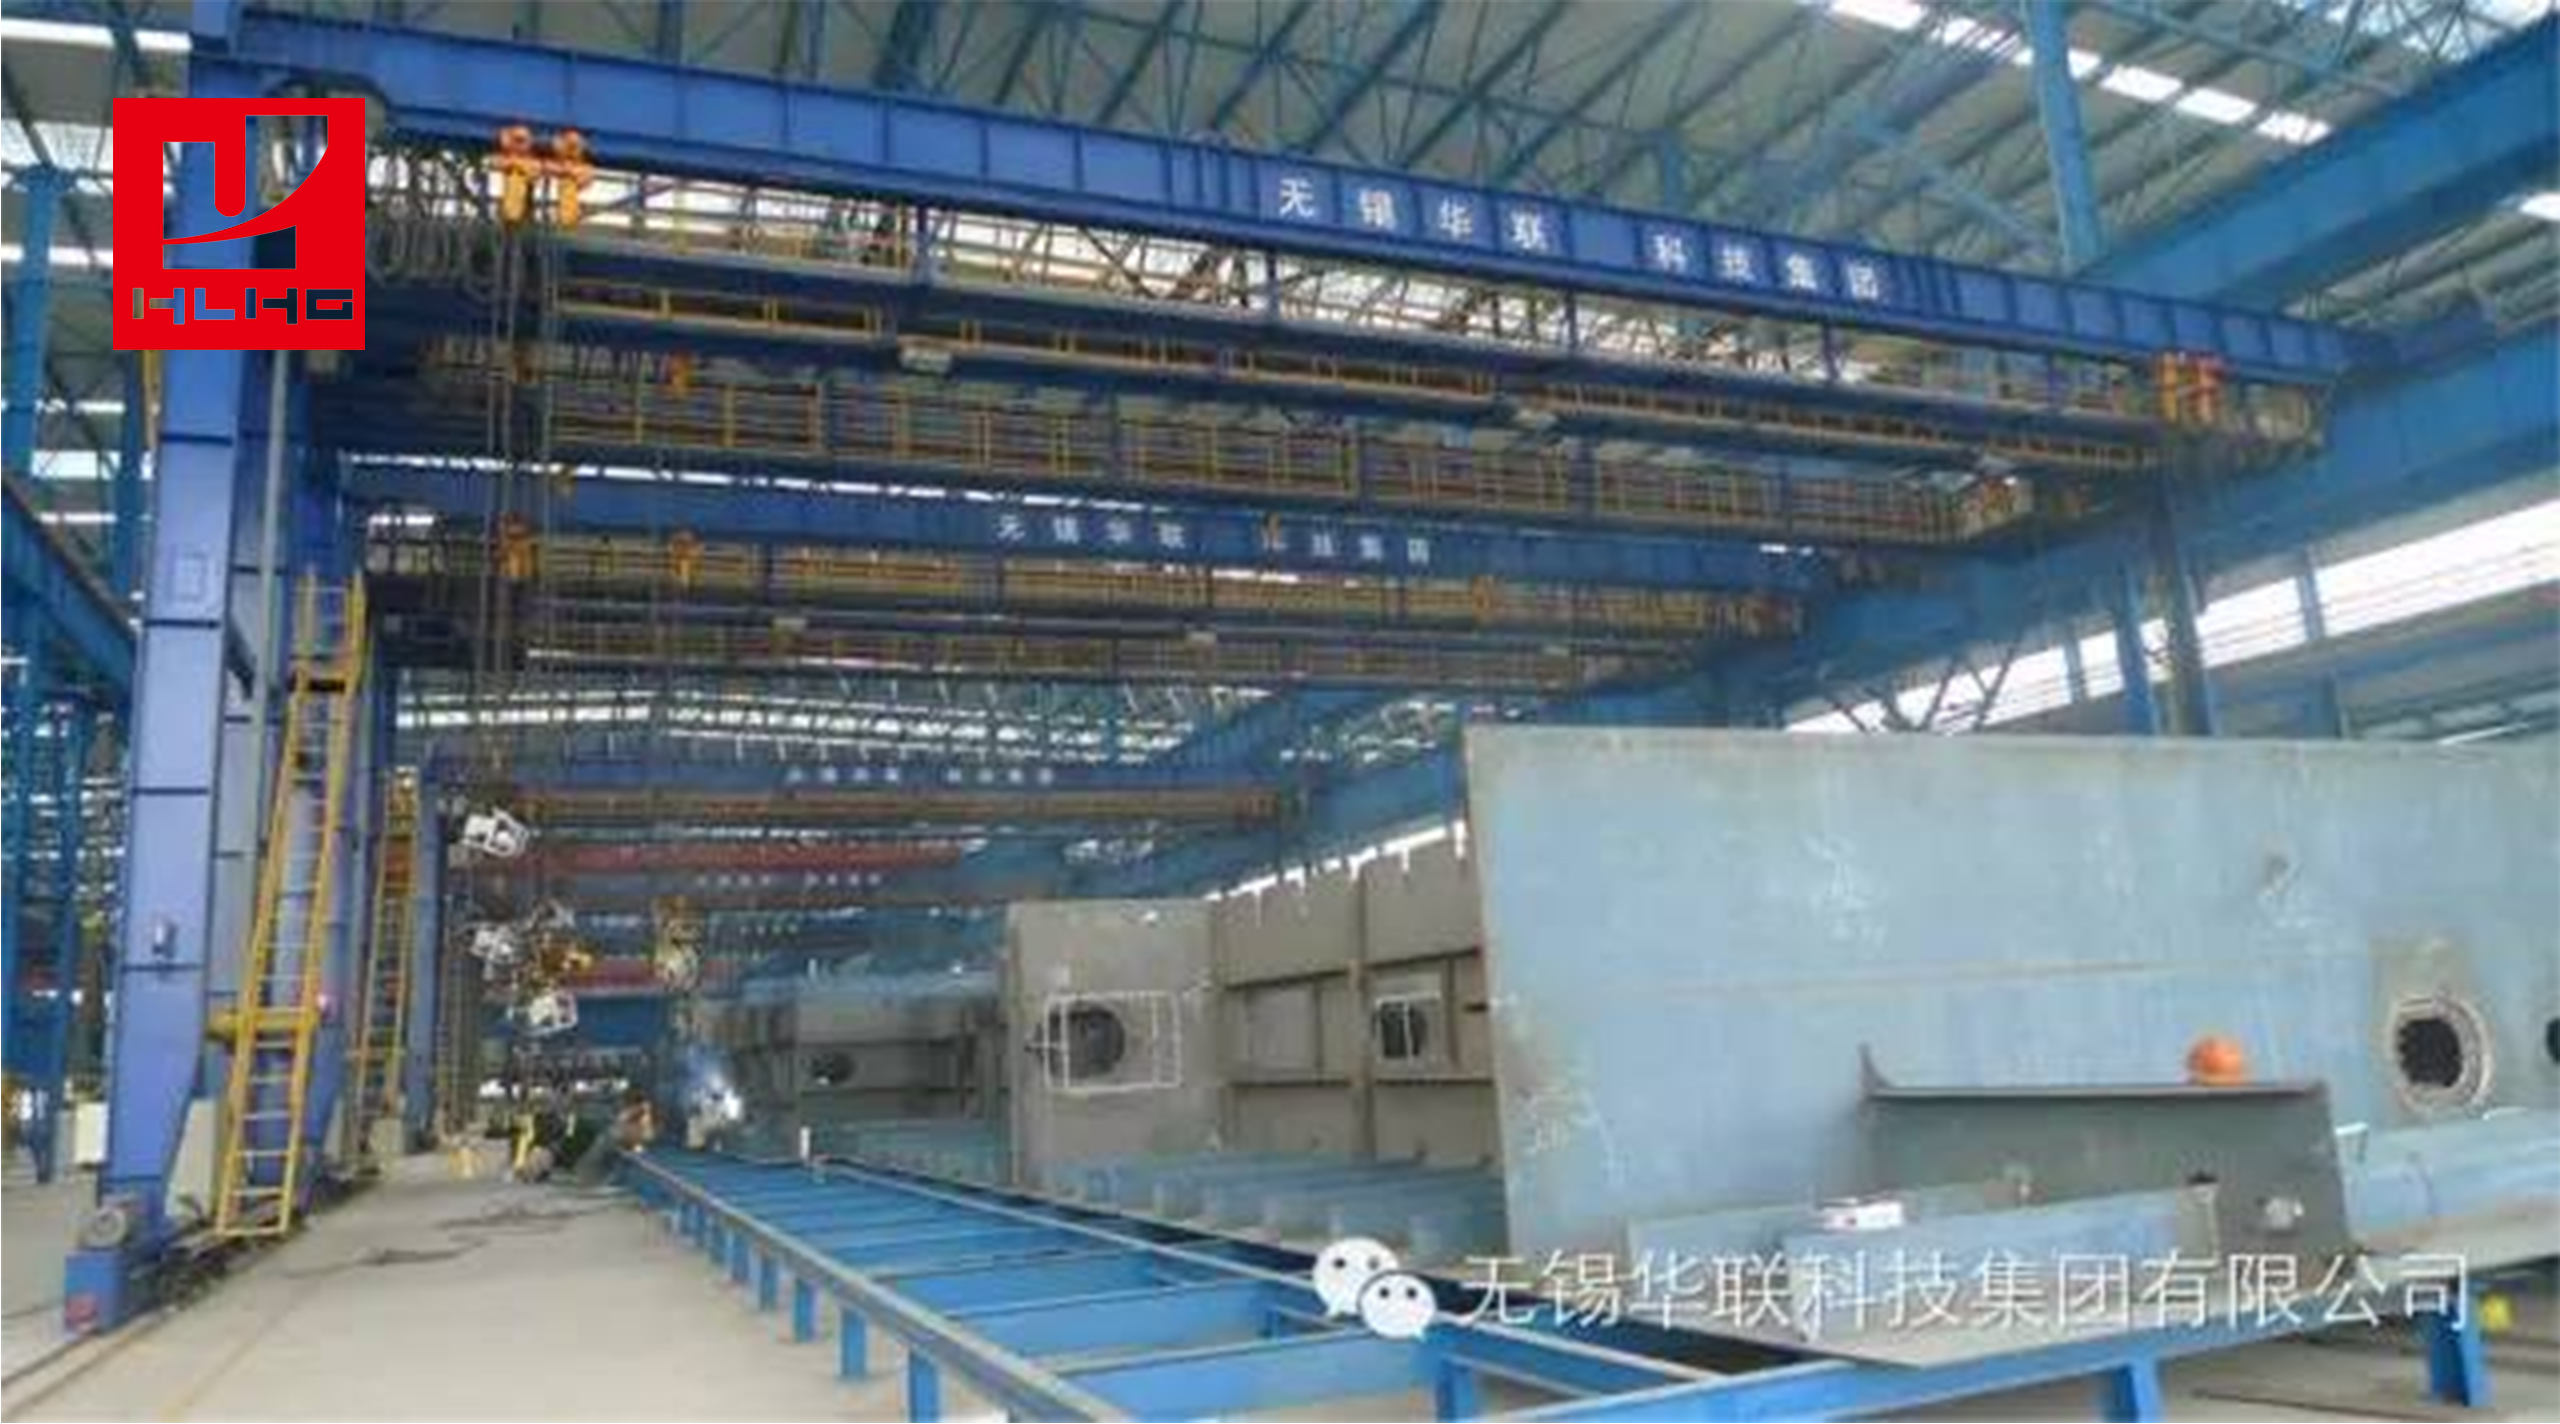
WUXI, JIANGSU, CHINA, September 29, 2026 /EINPresswire.com/ -- A modern ship panel production line connects complex fabrication stages into a synchronized manufacturing flow. Advancing shipyard production systems since its founding in 1987, Wuxi Hualian Science & Technology Group—recognized across international maritime markets as Hualian, structures panel fabrication around staged physical movement and quality verification. High-performance shipyard automation requires more than placing independent machinery in physical sequence. Each production handoff demands a verified workpiece, a documented quality status, and a receiving station ready for transfer. Establishing disciplined workflow handoffs prevents upstream fabrication defects from compounding into massive structural misalignment in downstream erection stages.
Define what crosses each handoff
A dependable production handoff requires transferring three critical project elements: verified physical geometry, structural workpiece identity, and documented inspection clearance. Material tracking systems must associate each plate assembly with its unique block allocation, steel specification, and approved construction drawings. Workpieces entering a downstream station must satisfy defined geometric tolerances. Overall panel width, plate thickness, stiffener spacing, and reference edge alignment must fall within tight millimeter limits. Handing over twisted or incorrectly aligned blanks forces downstream automated carriages to fault. Furthermore, each handoff marks an irreversible transition in structural value. Straightening distorted plate skins after welding transverse web frames is extraordinarily difficult and expensive. Validating joint geometry before advancing panels guarantees predictable downline flow.
Establishing standardized verification gates ensures that receiving workstations inherit structurally sound assemblies, eliminating costly disassembly and rework during subsequent block fitting. Digital identification tags linked to barcode scanners verify plate steel grades and thickness before automated welding arcs ignite, preventing accidental welding parameter mismatches. Maintaining datum consistency across transfers guarantees that robotically marked reference lines align perfectly with stiffener mounting locations. Laser distance meters and digital angle sensors mounted at transfer stations measure web plate squareness before assembly begins. Automated interlocking stops halt conveyor movement if plate diagonal measurements exceed project tolerance limits. Immediate automated feedback prevents out-of-square panels from entering welding gantries. Standardizing edge bevel profiles before transfer ensures uniform joint penetration during automated welding. Ultrasonic thickness gauges confirm plate gauge conformity, alerting operators if mill thickness tolerances deviate from engineering drawing specifications.
Keep inspection and repair inside the production route
Automated panel fabrication lines cannot assume zero defect rates. Welding imperfections, including localized porosity, slag inclusions, or incomplete root penetration, occasionally occur due to plate mill scale or voltage fluctuations. Standard shipyard panel lines integrate dedicated non-destructive examination and repair buffers directly between primary workstations. For example, positioning an inspection station immediately following single-sided plate butt welding enables technicians to perform ultrasonic and visual checks while the plate rests on motorized rolls. Minor weld defects can be ground out and repaired on-station using certified procedures before the plate receives longitudinal stiffeners. Containing quality control inside the line boundary prevents flawed assemblies from contaminating downstream assembly stages.
Integrating rapid defect remediation stations maintains unbroken manufacturing momentum, ensuring that structural hull blocks advance toward the dry dock without quality holds. Providing well-lit inspection access with overhead fume extraction empowers quality auditors to complete non-destructive examinations safely without stopping conveyor transit. Documenting inspection sign-offs electronically within the line database provides instant traceability required by visiting classification society surveyors. Providing motorized grind-out stations with integrated vacuum hoods allows welders to eliminate root flaws quickly without filling the bay with abrasive dust. Immediate local repair prevents defective panels from reaching downstream stiffener mounting bays.
Find the constraint in the work, not in the machine label
Manufacturing bottlenecks in shipyard panel bays rarely stem from torch travel speeds alone. Cycle times are primarily governed by manual fit-up complexity, crane availability, tack welding delays, and slag cleaning. Planners must calculate the true station balance across the entire bay. While an automatic multi-torch stiffener welder may travel at 800 mm per minute, loading and clamping twenty individual bulb flats requires substantial preparation time. Installing motorized infeed conveyors and automated stiffener loading arms balances line takt time. Aligning material handling speed with arc-on time ensures that capital-intensive welding gantries operate at maximum capacity.
Analyzing complete workstation cycle times prevents shipbuilders from purchasing oversized welding power sources when material handling speed is the true limiting factor. Buffer zones between butt welding, stiffener mounting, and web frame fitting absorb minor process variations, keeping high-value machines continuously operating. Stiffener tacking speed often dictates overall line cadence. Employing dedicated pneumatic clamping jigs accelerates tack welding cycles, allowing longitudinal stiffeners to be locked quickly. Mechanized clamping eliminates manual wedge driving, protecting plate surfaces from mechanical gouges. Staging longitudinal stiffeners in kitted sets beside the conveyor reduces crane waiting times. Forklift loading cassettes deliver pre-cut bulb flats directly to the operator platform, maintaining continuous feeding into hydraulic mounting gantries.
Separate physical coordination, machine settings and plant data
Designing robust production automation requires maintaining clear separation between three operational layers. The physical layer governs conveyor drives, alignment stops, hydraulic clamps, and mechanical interlocks that ensure worker safety. The process control layer manages digital welding power sources, seam tracking sensors, wire feed rates, and travel speeds. Programmable logic controllers store qualified welding parameters, ensuring repeatable heat input across varied steel grades. The plant data layer links the production line to shipyard planning systems. Nesting data, cutting schedules, and panel release records transfer electronically without requiring complex software integrations on individual machine controllers. Decoupling data communications from real-time motion control safeguards machinery reliability, preventing network latency from interrupting active submerged arc welding passes. Dedicated industrial fieldbus networks connect machine sub-panels without overburdening central plant servers. Isolated control loops guarantee millisecond-level responsiveness for critical safety stops and welding head position corrections. This robust architecture prevents communication delays during high-speed gantry travel.
Measure accepted flow against a consistent baseline
Shipyard productivity cannot be measured by gross tonnage alone. Delivering hundreds of tons of distorted panels that require weeks of flame straightening in the dry dock degrades shipyard profitability. Management teams should evaluate performance by accepted square meters of completed panel blocks delivered on schedule with zero defect rework. Synchronized automation delivers predictable throughput and reduces dry dock labor. Tracking defect-free block completions provides a true metric of factory efficiency, aligning machinery performance with overall shipyard delivery commitments. Tracking dimensional conformance through digital laser scans provides verifiable records for shipowners and classification societies. Consistent panel geometry accelerates erection dock turnover, maximizing annual shipyard vessel deliveries.
Shipbuilders planning panel line modernization can consult Hualian to configure balanced production workflows and automated equipment cells: https://www.hualianoversea.com/. Hualian provides comprehensive engineering designs that unite heavy machinery with dependable shipyard fabrication workflows.
Wuxi Hualian Science & Technology Group
Hualian
email us here
Visit us on social media:
YouTube
Legal Disclaimer:
EIN Presswire provides this news content "as is" without warranty of any kind. We do not accept any responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you have any complaints or copyright issues related to this article, kindly contact the author above.